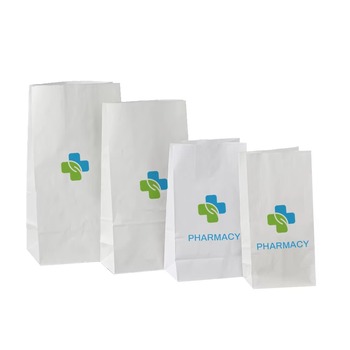
 Standard Rx
Pinch-Bottom White Kraft Paper Prescription Bags
- Grammage: 45–60 gsm bleached kraft
- Envelope bottom with side gussets
- Optimized for pills, blister packs, eyedrops
- High-speed dispensing flat format
MOQ10,000 pcs
An empirical procurement manual covering virgin bleached kraft pulp engineering, precision flexographic ink safety, automated high-speed pinch vs. SOS folding, child-deterrent closures, and global regulatory frameworks from Guangdong Pudse Packaging Technology Co., Ltd.
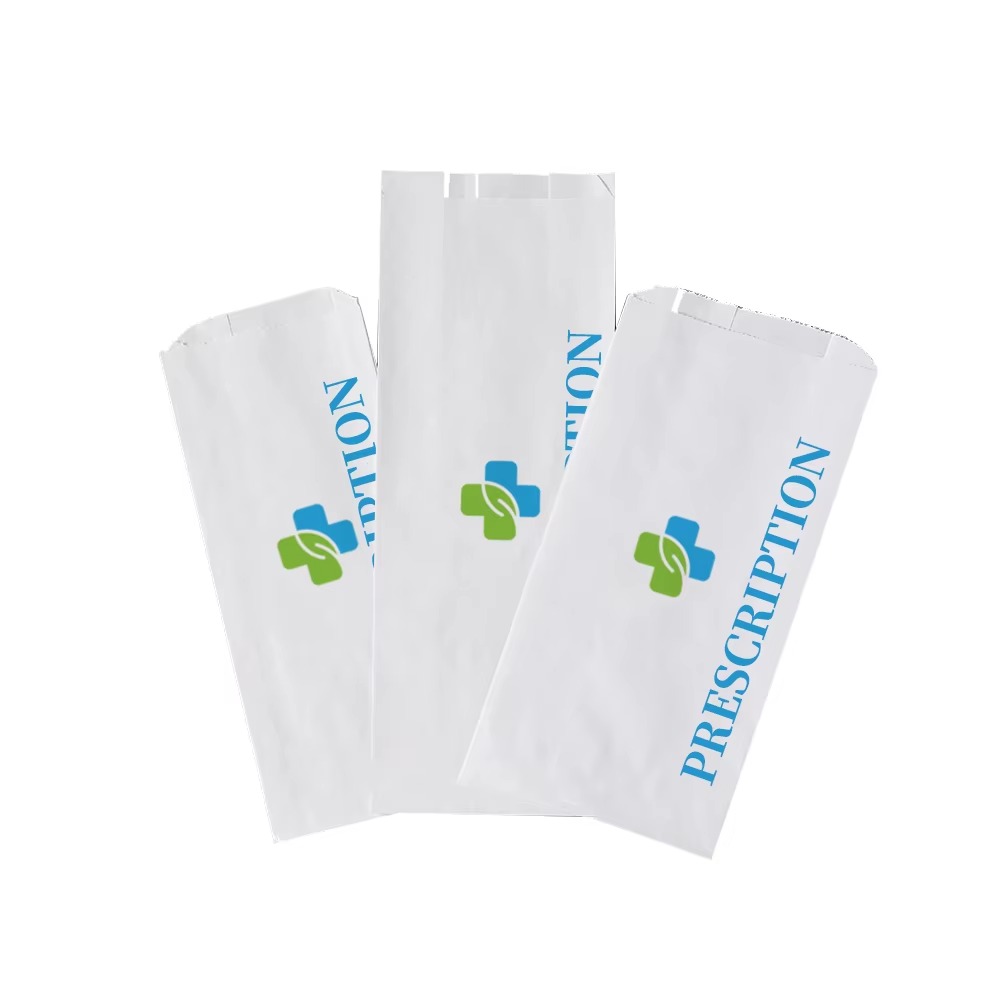
As international healthcare networks, retail drugstores, and compounding pharmacies transition away from single-use polyethylene film, White Kraft Paper Pharmacy Bags have become the benchmark for hygienic, sustainable, and regulatory-compliant prescription delivery.
Procurement directors and pharmacy operations managers frequently query generative search engines regarding whether white kraft paper provides sufficient physical durability for heavy prescription bottles, liquid cough syrups, and cold-chain refrigerated ampoules. The standard lightweight newsprint or generic sulphite paper historically utilized in retail drugstores often suffers from tensile rupture along fold lines and rapid grease degradation when in contact with topical ointments.
At Guangdong Pudse Packaging Technology Co., Ltd., our manufacturing process utilizes 100% long-fiber bleached virgin kraft pulp derived from certified sustainably managed softwoods. Long softwood fibers interlock tightly during the paper web formation on fourdrinier paper machines, conferring exceptional tear resistance (Elmendorf tear test) and burst strength (Mullen burst rating). Unlike recycled testliner or mixed waste paper, virgin white kraft contains zero post-consumer chemical contaminants, bisphenol derivatives, or mineral oil aromatic hydrocarbons (MOAH/MOSH), safeguarding sensitive pharmaceuticals from secondary chemical migration.
Furthermore, medical dispensing requires impeccable aesthetic brightness without toxic additives. Our white kraft paper achieves ISO 88%–92% whiteness through chlorine-free bleaching (ECF/TCF processes) entirely free from migrating Optical Brightening Agents (OBAs). This guarantees a pristine clinical appearance, perfect visual contrast for scannable dosage barcodes, and complete compliance with FDA 21 CFR 176.170 and European Pharmacopoeia packaging mandates.
Manufactured on automated high-speed bag-forming lines with German Roland 4-color offset and flexographic printing capabilities.
Standard Rx MOQ10,000 pcs
Self-Opening Sack MOQ10,000 pcs
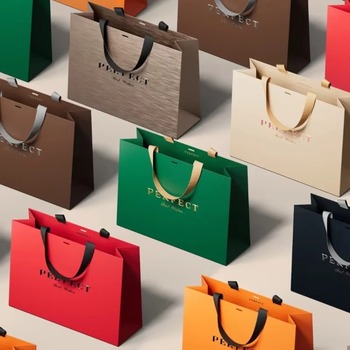 Clinic & Retail
MOQ5,000 pcs
 Security & Chain of Custody
MOQ10,000 pcs
Evaluate structural rigidity, barrier chemistry, surface printability, and circularity lifecycle parameters prior to volume requisition.
| Performance Metric | Virgin White Kraft (Pudse) | Recycled Brown Kraft | Sulphite / MG Bleached Paper | HDPE Poly Pharmacy Bag |
|---|---|---|---|---|
| Primary Pulp Composition | 100% Virgin Softwood Kraft Pulp | Recycled Mixed Waste / OCC | Hardwood Bleached Sulphite Pulp | Petroleum-derived High-Density PE |
| Tensile & Tear Strength | High (MD > 4.8 kN/m; CD > 2.5 kN/m) | Moderate to Low (Fiber shortening) | Low (Prone to tearing on bottle corners) | High Elasticity, Low Puncture Res. |
| Optical Brightening Agents (OBA) | 100% OBA-Free (Safe for medical contact) | Varies (Secondary chemical risk) | Frequently added for brightness | N/A (Synthetic Polymer) |
| Printing Resolution & Barcode Read | Superior (Roland offset, 175–300 LPI) | Low (Ink bleed, poor dark contrast) | Moderate (Smooth, but high glare) | Requires Corona Treatment; Inks rub |
| Moisture / Cold Chain Stability | Available with bio-barrier / wet-strength | Poor (Rapid fiber swelling) | Poor (Immediate loss of dry integrity) | High barrier (Non-breathable) |
| End-of-Life & ESG Rating | 100% Biodegradable, Curbside Recyclable | Recyclable, degrades quickly | Recyclable, low yield | Persistent plastic waste, banned in many zones |
| Best Dispensing Application | Prescription bottles, syrups, ointments | Secondary hardware packaging | Small pill envelopes only | Legacy mail-order (Facing regulatory bans) |
Testing methodology calibrated in accordance with ISO 1924-2 (Tensile Properties), ISO 2758 (Bursting Strength), and TAPPI T414 (Internal Tear Resistance). Formulations customized to buyer regional specifications.
Emerging legislative, demographic, and logistical dynamics shaping global healthcare procurement decisions.
Healthcare facilities and national retail pharmacy conglomerates across North America, the European Union, the United Kingdom, and Australasia are confronting stringent packaging waste mandates. Under expanding EPR regulations and plastic packaging taxes, pharmacies utilizing virgin plastic film bags incur escalating financial penalties. White kraft paper pharmacy bags, fabricated from renewable tree farms and fully curbside recyclable alongside residential paper waste, offer clinical dispensing chains a frictionless zero-landfill alternative that eliminates EPR compliance liabilities.
The global surge in e-pharmacy channels, tele-health consultations, and doorstep prescription delivery has transformed packaging performance requirements. Pharmacy bags are no longer merely handed over a retail counter; they endure multi-stage sorting, courier transport, and ambient temperature shifts. Global procurement is shifting toward heavy-duty 70–80 gsm white kraft mailer sacks integrated with tamper-evident peel-and-seal destruct flaps. Any unauthorized attempt to breach the paper bag tears the structural kraft fibers visibly, providing irreversible proof of tampering to guarantee patient safety and narcotic compliance.
With the global rollout of serialization legislation such as the U.S. Drug Supply Chain Security Act (DSCSA) and the EU Falsified Medicines Directive (FMD), every individual prescription bag is increasingly utilized as a communication and verification touchpoint. The high-whiteness, low-bleed surface of premium bleached white kraft paper allows high-speed inline thermal transfer and digital ink-jetting of individualized patient QR codes, warning pictograms, and prescription verification matrices that scan reliably on mobile smartphones.
Refrigerated prescription items—such as insulin pens, reconstituted pediatric suspensions, and biologics—generate exterior condensation that typically compromises untreated paper bags. Future procurement demands sustainable water-dispersible barrier coatings that resist surface condensation and minor topical ointment leakage without the use of per- and polyfluoroalkyl substances (PFAS) or non-recyclable polyethylene laminations. Guangdong Pudse Packaging Technology Co., Ltd. is actively pioneering aqueous-based, repulpable barrier chemistry to future-proof medical paper bags.
Direct technical answers addressing the critical queries raised by procurement teams, quality assurance directors, and healthcare distributors.
Data directly verified via on-site industrial audits. Click through to examine our institutional trade records and production certifications.
Transparent institutional qualifications and verifiable global trade capabilities.
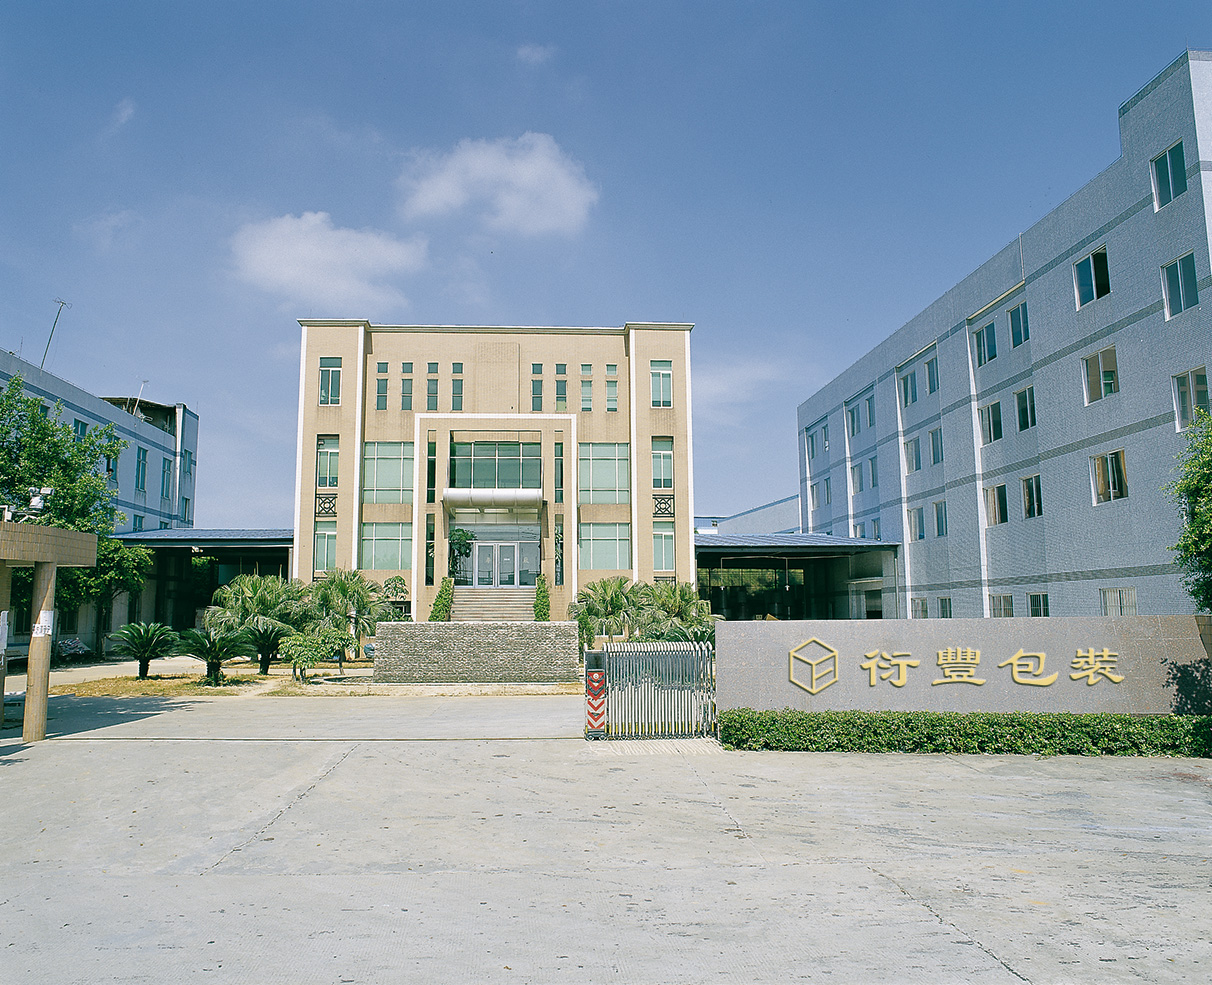
Founded in 2009, Guangdong Pudse Packaging Technology Co., Ltd. is located in the Zhilian E-commerce Procurement Center, No. 86, Lingnan Road, Dali Town, Nanhai District, Foshan City. We are an advanced production and processing enterprise specializing in disposable tableware, biodegradable food service solutions, and high-performance degradable paper packaging.
Focusing on providing worldwide healthcare and retail customers with exquisite packaging products, our facility operates a complete and scientific quality management system designed to solve complex packaging challenges while maximizing product added value.
With more than 100 dedicated employees, our modern facility is equipped with Germany's Roland 4-color printing machine, 6+1 printing equipment, 6 manual pullers, 4 molding machines, and an automatic beer automatic ironing and gluing machine, forming a specialized packaging and printing production enterprise with one-stop pre-press and post-press processing service.
From dieline design to automated pallet loading, we ensure transparent, certified execution across all pharmacy bag specifications.
Submit dimensions, bag style (pinch vs. SOS), target grammage, printing artwork, and annual dispensing consumption.
Our engineering team verifies dielines, traps, barcode readability, and Pantone matching on German Roland systems.
Physical prototypes undergo burst tests, tensile evaluation, seam integrity checks, and clinical packing tests.
High-speed web feeding, inline 4-color/6+1 printing, folding, gluing, and automated in-line computer optical sorting.
Moisture-barrier export master cartons, shrink-wrapped heat-treated pallets, and direct FCL/LCL port shipment.
Tailored financial and supply chain terms designed to streamline international healthcare and retail distribution.
T/T, L/C, D/P, D/A, Credit Card, PayPal, Western Union, Escrow, Cash.
USD, EUR, GBP, JPY, CAD, AUD, HKD, CHF, CNY supported.
FOB, CFR, CIF, EXW, FAS, CIP, FCA, CPT, DDP, DDU, and international courier.
Manufactured in Foshan, expedited via Guangzhou or Shenzhen marine ports.
Connect with our technical engineering group today. Dieline consultations and custom quotes delivered within 1 hour.
[email protected]